 CN
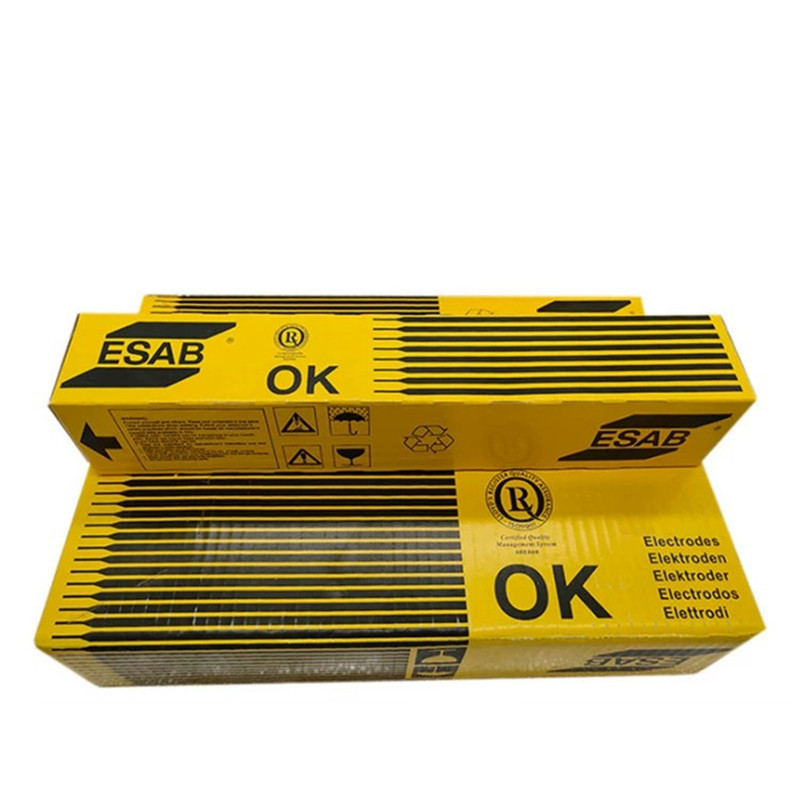
ESAB OK 55.00 (E7018-1 H4 R): A Low-Hydrogen Carbon Steel Electrode Built for Tough Jobs
When a weld has to hold under stress, impact and low temperatures, the electrode you choose decides whether the joint passes inspection or fails it. The ESAB OK 55.00 — a Swedish-made, AWS A5.1 E7018-1 H4 R low-hydrogen carbon steel electrode — is one of the most trusted answers to that challenge. Manufactured in Sweden by ESAB, a name that has defined welding quality for more than a century, OK 55.00 delivers a combination of strength, ductility and arc stability that general-purpose electrodes simply cannot match.
In this guide we break down what makes OK 55.00 different, how to weld with it, where it belongs on your project, and what buyers in Africa and other export markets need to know before ordering.
Product Snapshot
| Attribute | Detail |
|---|---|
| Brand | ESAB (Sweden) |
| Model / Classification | OK 55.00 – AWS A5.1 E7018-1 H4 R |
| Article Number | 076762 |
| Type | Low-hydrogen, iron powder, basic covered carbon steel electrode |
| Country of Origin | Sweden (imported) |
| Diameter Range | 2.5 mm – 4.0 mm |
| Welding Positions | All positions (flat, horizontal, vertical, overhead) |
| Current | AC / DC (electrode positive recommended) |
| Certification | AWS A5.1; RoHS compliant |
| Hydrogen Content | H4 – max. 4 ml/100 g diffusible hydrogen |
| Availability | Cross-border export stock, wholesale quantities |
Why the E7018-1 H4 R Classification Matters
Every character in the classification tells you something about performance:
- E70 — minimum tensile strength of 70,000 psi (about 490 MPa) in the as-welded condition.
- 1 — the 1 suffix guarantees a minimum impact energy of 27 J at −46 °C, making this electrode suitable for low-temperature service where ordinary E7018 would fall short.
- H4 — diffusible hydrogen is capped at just 4 ml per 100 g of deposited metal, drastically reducing the risk of hydrogen-induced cold cracking in thick sections and high-restraint joints.
- R — a moisture-resistant coating, which means the electrode can tolerate short-term exposure to humid air without a serious drop in weld quality. This is a real advantage in tropical climates and on outdoor sites.
For structural steelwork, pressure vessels, bridge components and heavy machinery, that combination is exactly what inspectors want to see on the certificate.
Performance Highlights
1. Exceptional Arc Stability
OK 55.00 strikes easily, re-strikes without sticking, and maintains a smooth, quiet arc even on AC power supplies or long extension cables. Welders working with generator sets in remote locations will notice the difference immediately.
2. Clean, Spatter-Free Beads
The iron-powder basic coating produces a finely rippled bead with self-releasing slag and minimal spatter. Cleanup time drops, and the finished weld looks as good as it performs.
3. Excellent Mechanical Properties
Typical all-weld-metal results include tensile strength around 550–600 MPa, yield strength above 460 MPa, elongation of 25% or more, and Charpy V-notch impact values that comfortably exceed 27 J at −46 °C. That margin of safety matters on critical structures.
4. Low-Hydrogen Security
With H4 classification, OK 55.00 is well suited to welding medium- and high-carbon steels, thick plate, and joints with high restraint — situations where cold cracking is a genuine risk with rutile or cellulose electrodes.
5. All-Position Versatility
From flat butt welds to vertical-up and overhead fillets, the electrode keeps a stable arc and consistent deposition. One electrode covers the whole job, which simplifies inventory and reduces downtime.
Recommended Welding Parameters
| Diameter | Current Range (AC/DC) | Typical Applications |
|---|---|---|
| 2.5 mm | 70 – 110 A | Root passes, thin plate, vertical and overhead work |
| 3.2 mm | 110 – 150 A | General structural welding, fill and cap passes |
| 4.0 mm | 150 – 200 A | Heavy plate, thick sections, high-deposition flat welding |
Storage tip: Although the R coating resists moisture, best practice is to keep electrodes in a dry store and re-bake at 300–350 °C for 1–2 hours if they have been exposed to damp conditions. This preserves the H4 hydrogen level and protects your weld quality.
Where OK 55.00 Belongs on Site
- Structural steel fabrication — beams, columns, bracing and connections
- Pressure vessels and boilers requiring impact-tested joints
- Bridges, cranes and lifting equipment
- Shipbuilding and offshore structures in low-temperature service
- Heavy machinery, mining equipment and repair welding on carbon and low-alloy steels
- Pipe welding where hydrogen control is critical
Export and Wholesale Supply
This product is offered as a cross-border export stock item, with bulk availability for distributors, fabricators and project contractors. It is supplied in original ESAB packaging from Sweden, with traceability on the article number 076762. Shipping and export documentation can be arranged for welding consumables cargo, including customs clearance support for import/export of welding materials.
Popular sales channels include Baidu, Taobao, Pinduoduo, 1688/Ai Caigou, Amazon, AliExpress, Lazada, Shopee, Wish, Temu and independent stores — with strong demand across African markets where durability and cost-per-meter performance are decisive factors. RoHS compliance makes the electrode suitable for markets with strict environmental requirements.
Ordering Checklist
- Confirm the diameter you need (2.5 mm, 3.2 mm or 4.0 mm).
- Specify quantities in kilograms or cartons for wholesale pricing.
- Check power supply on site — OK 55.00 runs on both AC and DC, but DC+ gives the best arc characteristics.
- Request the mill certificate and AWS compliance documentation if the project requires traceability.
- Plan storage to protect the electrode coating from humidity before use.
Final Thoughts
The ESAB OK 55.00 E7018-1 H4 R is not the cheapest electrode on the shelf — it is the one that keeps your weld from failing inspection. For fabricators working with thick carbon steel, low-temperature service conditions, or high-restraint joints, the H4 hydrogen rating and −46 °C impact guarantee pay for themselves the first time a critical test is passed.
Made in Sweden, AWS certified, RoHS compliant and available for export in wholesale volumes — it is a dependable addition to any serious welding consumables inventory.